Introduction
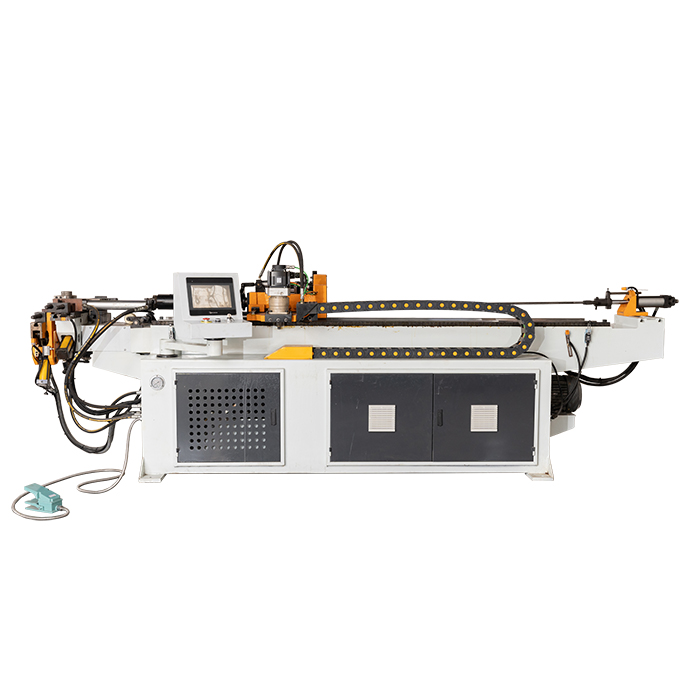
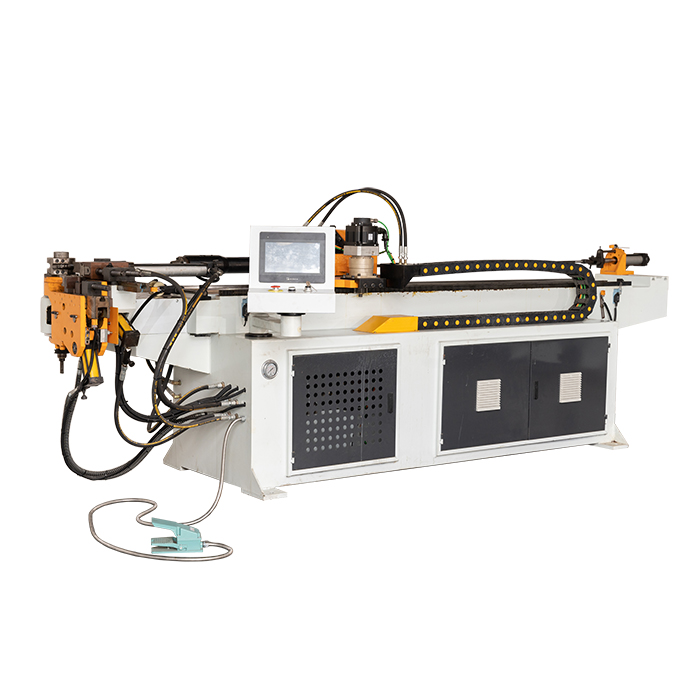
Tube bending is an important process in metal pipe fabrication. It allows manufacturers to create curved tube parts for different industrial products, including furniture frames, automotive components, gym equipment, handrails, motorcycle parts, bicycle frames, and customized metal structures.
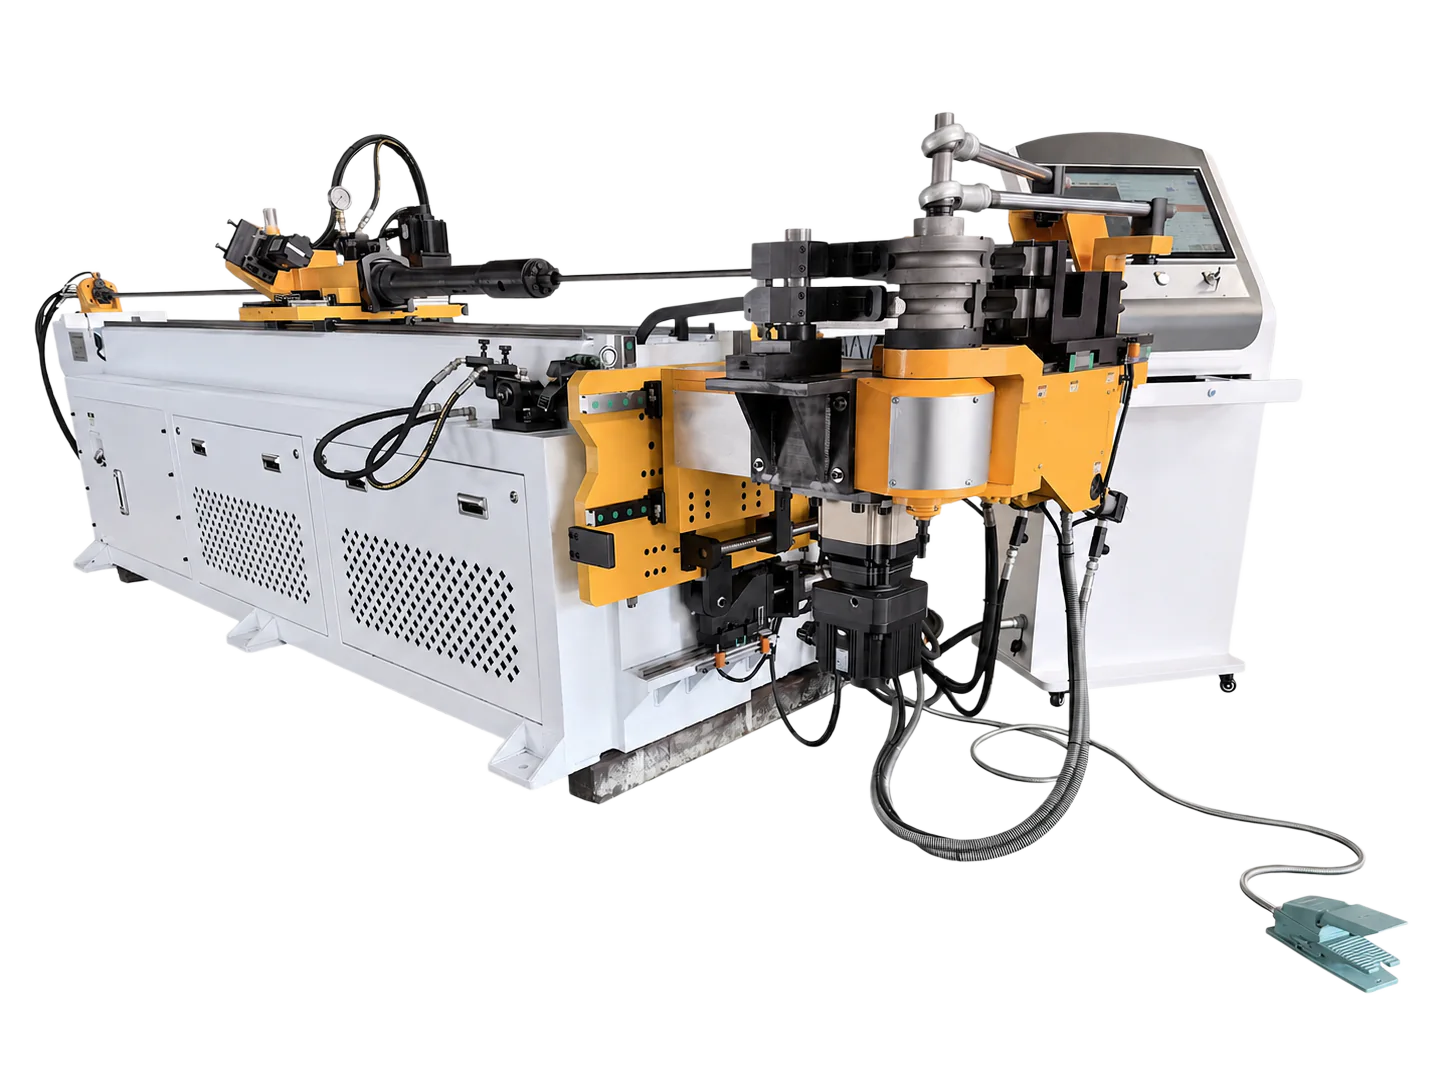
However, tube bending is not only about bending a pipe to a certain angle. A good bending result depends on tube material, wall thickness, bending radius, tooling design, machine stability, clamping force, and process control.
If the machine or tooling is not suitable, problems may appear during production. These problems can affect product appearance, assembly accuracy, structural strength, and production efficiency.
1. Tube Wrinkling
Tube wrinkling is one of the most common problems during bending. It usually appears on the inner side of the bend.
Common causes include a bending radius that is too small, thin tube wall thickness, insufficient internal support, incorrect tooling design, poor clamping or pressure control, and unsuitable material for tight-radius bending.
To reduce wrinkling, manufacturers should choose the proper bending radius according to the tube diameter and wall thickness. For thin-wall tubes or small-radius bending, mandrel support may be required. Suitable pressure dies and wiper dies can also help control material flow during bending.
2. Tube Cracking
Tube cracking usually happens on the outer side of the bend because this area is stretched during bending.
Common causes include poor material ductility, a bending radius that is too small, unsuitable wall thickness, surface defects on the tube, incorrect bending speed, and wrong tooling selection.
Before bending, it is important to confirm the tube material and its forming ability. For harder materials such as stainless steel or high-strength carbon steel, the bending radius should not be too small. Sample testing before mass production can help reduce risk.
3. Tube Flattening
Tube flattening means the tube loses its original round shape during bending. This problem affects both appearance and structural strength.
Common causes include a tight bending radius, thin tube wall thickness, lack of mandrel support, incorrect pressure die setting, insufficient machine rigidity, and tooling that does not match the tube size.
To prevent flattening, the bending die should match the tube diameter accurately. Thin-wall tubes often require mandrel bending to support the inside of the tube. A stable bending head and strong clamping system are also important.
4. Springback
Springback means the tube slightly returns after bending, causing the final angle to be different from the programmed angle.
Common causes include material elasticity, stainless steel or high-strength materials, incorrect bending angle compensation, inconsistent tube material, and unstable machine control.
Springback is normal in metal tube bending, but it must be controlled. CNC pipe bending machines can store bending programs and compensation values, helping improve repeatability in batch production.
5. Unstable Bending Angle
Unstable bending angle means each part may have slight differences, which can affect assembly and final product quality.
Common causes include unstable machine structure, inconsistent clamping force, inaccurate feeding, unstable hydraulic or servo control, non-standard operator settings, and tube material variation between batches.
To improve bending consistency, manufacturers should use a stable machine structure, reliable feeding system, and accurate control system. For batch production, CNC control is recommended.
6. Surface Scratches
Surface scratches are common when processing stainless steel, aluminum, or decorative tubes.
Common causes include rough tooling surfaces, metal chips or dust on the tooling, incorrect clamping pressure, poor lubrication, and direct friction between the tube and die.
To reduce surface scratches, tooling should be polished and cleaned regularly. For stainless steel or aluminum tubes, protective film or proper lubrication may be used. Tooling quality and maintenance are especially important for products with high appearance requirements.
7. Tube Deformation at the End
Sometimes the tube end becomes deformed after bending, especially when the bending position is too close to the tube end.
Common causes include insufficient clamping length, thin wall thickness, lack of tooling support, and incorrect feeding position.
Before production, the tube length and bending position should be checked carefully. If the bend is close to the tube end, special tooling or longer clamping allowance may be required.
8. Poor Repeatability in Batch Production
Poor repeatability means the first sample may be acceptable, but later parts are not consistent.
Common causes include manual operation differences, imprecise machine control, worn tooling, material variation, lack of standard production settings, and insufficient quality inspection during production.
For repeat production, CNC pipe bending machines are better than manual or semi-automatic machines. CNC systems can store programs and reduce operator error. Regular tooling inspection and machine maintenance also help ensure stable production quality.
Why the Right Pipe Bending Machine Matters
Many tube bending problems are caused by choosing the wrong machine or using unsuitable tooling. A professional pipe bending solution should be selected according to tube diameter, wall thickness, tube material, tube shape, bending radius, bending angle, product drawing, production quantity, and accuracy requirements.
DUORUI MACHINERY provides pipe bending machines and customized pipe processing solutions for different applications. With proper machine selection, tooling design, and process support, manufacturers can improve bending quality and reduce production problems.
Conclusion
Tube bending problems such as wrinkling, cracking, flattening, springback, unstable angles, scratches, and deformation can affect product quality and production efficiency. Most of these problems can be reduced by using the right machine, proper tooling, suitable bending radius, stable clamping, accurate control, and professional process testing.
Before purchasing a pipe bending machine, buyers should provide tube size, wall thickness, material, bending radius, bending angle, product drawings, and production requirements. This information helps the supplier recommend the correct machine model and tooling solution.
A reliable pipe bending solution is not only about bending the tube. It is about achieving stable, repeatable, and high-quality tube processing for long-term production.
Buyer Information Checklist
Tube size — Outer diameter, wall thickness, tube shape, and length. — Helps DUORUI recommend a suitable machine and tooling solution.
Material — Carbon steel, stainless steel, aluminum, copper, galvanized tube, or other materials. — Helps DUORUI recommend a suitable machine and tooling solution.
Bending requirement — Bending angle, bending radius, number of bends, and bend positions. — Helps DUORUI recommend a suitable machine and tooling solution.
Product drawing or sample — 2D/3D drawing, sample photo, or finished part requirement. — Helps DUORUI recommend a suitable machine and tooling solution.
Production target — Daily or monthly output, batch size, and automation requirement. — Helps DUORUI recommend a suitable machine and tooling solution.
Customization needs — Voltage, control language, tooling, mandrel support, loading/unloading options, and special requirements. — Helps DUORUI recommend a suitable machine and tooling solution.